Stainless cutting data needs an identified grade, material condition and tool series. Use those details to select the source cutting speed and tooth feed, then calculate RPM and linear feed. Keep the first-cut observations with that setup so a later grade or tooling change is not judged against an incomplete record.

Identify the stainless family
Austenitic, ferritic, martensitic and precipitation-hardening grades can machine differently. Work-hardening tendency, hardness and heat retention should be part of the machining plan. Record the exact grade whenever available.
Use the actual tool documentation
Stainless cutting data is strongly affected by carbide grade, coating, flute geometry and edge preparation. Start with the exact tool family rather than a generic “carbide end mill” value.
Calculate RPM
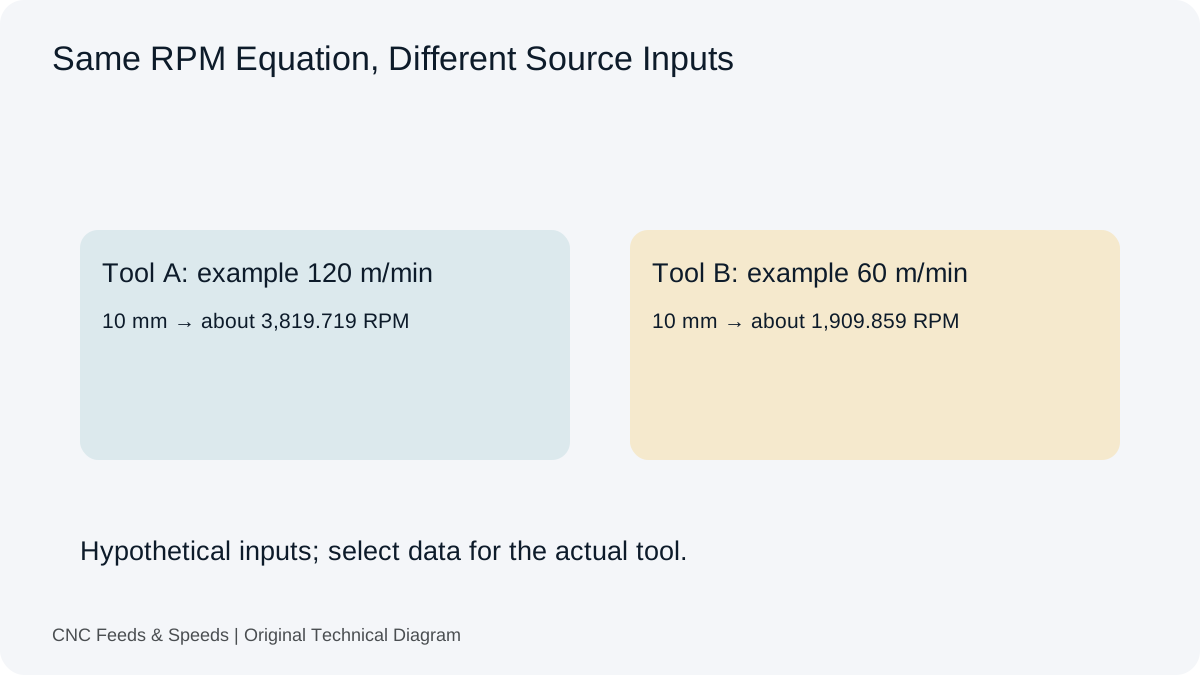
Use metric cutting speed or SFM with the actual cutter diameter. Verify the result against the machine spindle range. Check the cutting-speed recommendation separately from feed and toolpath contact; a spindle-speed value alone does not diagnose rubbing or work hardening.
Calculate feed from chip load
Once RPM is set, feed = RPM × flute count × chip load. Preserve the chip-load assumption when evaluating the result. If feed is reduced sharply without a corresponding reason, the tool may produce thinner chips and generate more heat.
Example
A 12 mm, 4-flute cutter using a hypothetical 90 m/min starting speed gives RPM ≈ 2,387. At 0.035 mm/tooth the feed is about 334 mm/min. These numbers illustrate the equations only; select the actual cutting data from a valid tool/material source.
Rigidity matters
Long stick-out, weak workholding or a thin wall can force a different process even when the arithmetic is correct. Chatter and deflection can appear before spindle power becomes the dominant limitation.
Avoid work-hardening traps
Interrupted dwell, rubbing and poor edge engagement can harden some stainless surfaces. Maintain a controlled cut and ensure the tool is actually removing material instead of sliding across the work.
Coolant and chip evacuation
Heat management and chip evacuation need to match the tool and machine. Flood, through-tool coolant, air or minimum-quantity strategies have different capabilities. The calculator does not model coolant delivery.
Tune deliberately
Change one variable at a time and watch chip shape, load, finish, burrs and tool wear. Record what changed so that the final condition is reproducible.
Practical stainless-steel record
Record the exact grade, hardness or heat-treatment condition when known, together with the tool geometry, coating, reach, coolant method and engagement. Stainless setups benefit from consistent documentation because a change in material condition can alter the result even when the tool and nominal dimensions are unchanged.
During validation, inspect the chips and the tool after a controlled cut. Look for evidence of rubbing, edge damage, built-up material, excessive heat or unstable cutting. Those observations help separate a tooling issue from a pure arithmetic issue.
Final verification
Keep the proven condition as a complete record rather than a single RPM or feed number. Future users should be able to see where the values came from and which setup assumptions were present when the result was proven.
Frequently asked questions
Why is stainless difficult to machine?
Its strength, heat behavior and work-hardening characteristics can make poor cutting conditions more damaging than the arithmetic suggests.
Should I use the same chip load across stainless grades?
Not automatically. Use data for the exact grade and tool.
Does lowering feed always reduce tool load?
It reduces programmed feed, but an excessively low chip thickness can increase rubbing and heat in some conditions.
Use Outokumpu Core and Forta product information for producer grade context. The stainless reference distinguishes that identification task from tool-specific cutting-data selection.
Help Improve This Resource
Request A Tool
Describe the calculation your workflow needs, the inputs you already have and the output you want to check. Include units and an example without confidential job details.
Request A ToolReport An Error
Share this page address, the entered values and the result you expected. Include the source of your comparison so the formula, units and explanation can be investigated.
Report An ErrorCNC Feeds & Speeds Editorial Desk
The site brings calculation tools and machining references into one workspace. Use the editorial and site information to understand its purpose and limitations. Send corrections with a reproducible example through the error report form.