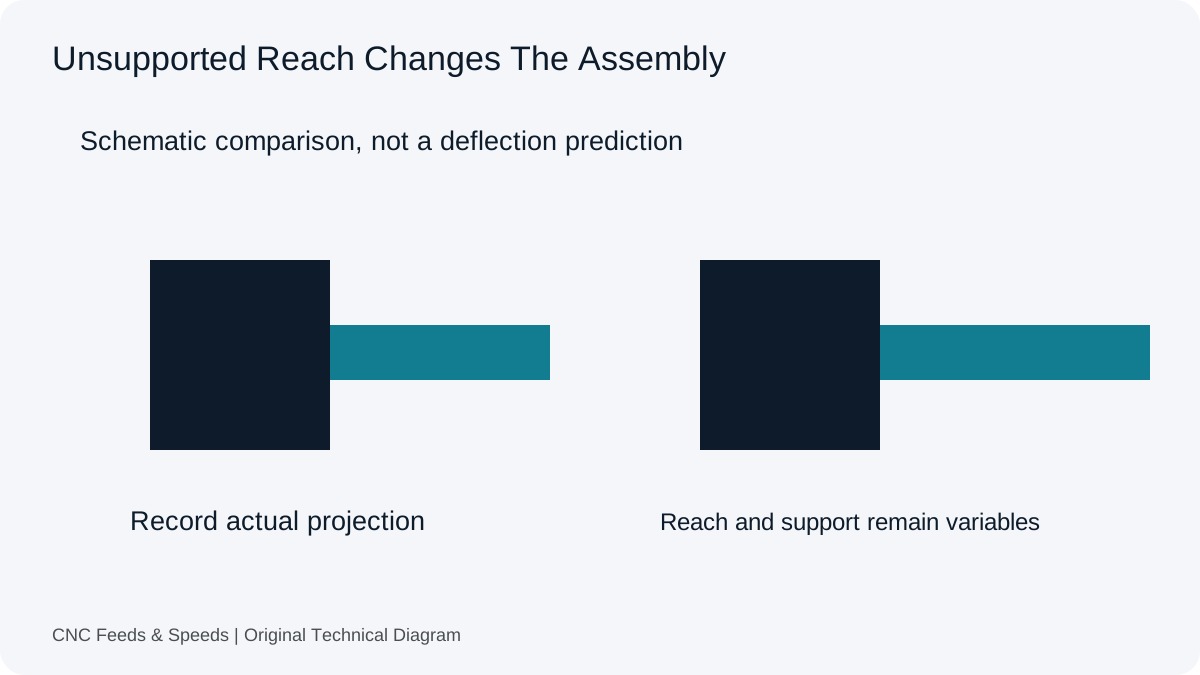
Tool stick-out is the unsupported extension from the holder toward the cutting region. Increasing that extension can reduce stiffness and change stability even when programmed RPM and feed remain the same. Chatter diagnosis therefore needs the toolholding, workpiece support and engagement recorded alongside the calculation.
Why stick-out changes the process
A longer unsupported tool deflects more under the same cutting force. The relationship is strongly non-linear in many practical tool setups, so a small increase in unsupported length can produce a noticeable loss of stiffness.
Start with the shortest practical tool
Use only the reach needed to clear the feature while maintaining access. A longer tool may be required for deep pockets, but unnecessary extension adds a source of instability before any calculator value is changed.
Chatter is a system problem
Chatter can involve the tool, holder, spindle, workholding, part geometry or cutting condition. Do not assume that a speed change is the only solution. First inspect whether the tool is held securely, whether the workpiece is supported, and whether runout or excessive reach is present.
Use cutting data as a controlled variable
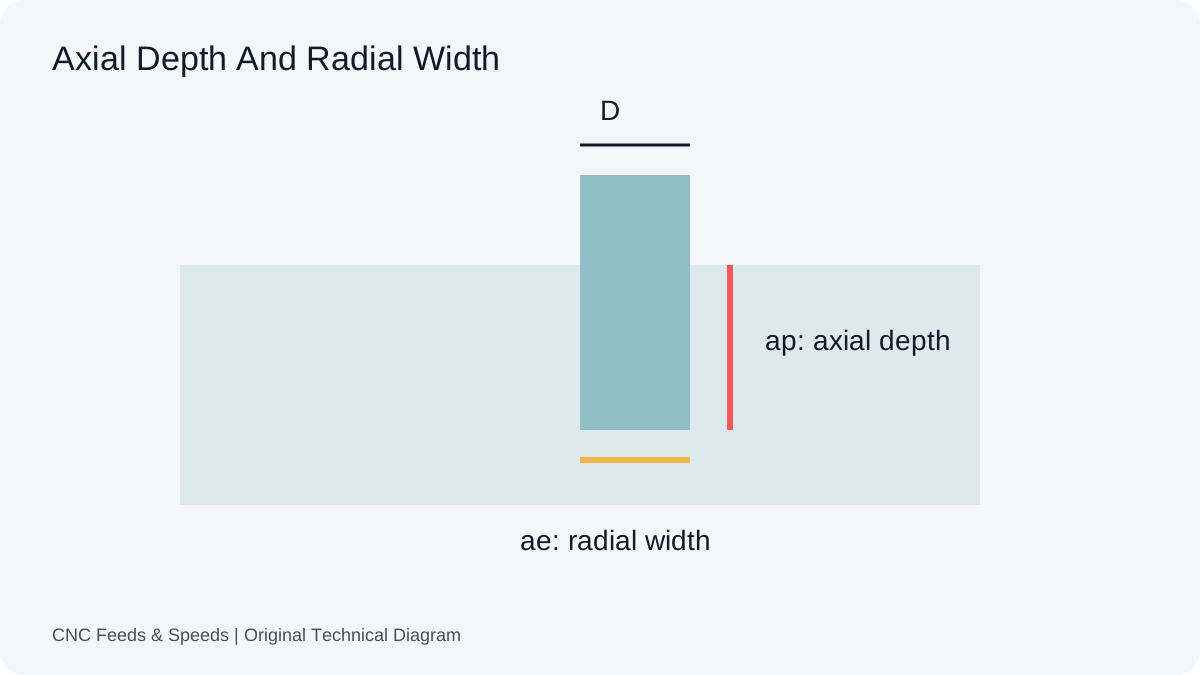
When troubleshooting, preserve the calculated relationship and change one variable. For example, reduce radial engagement or adjust spindle speed according to a validated strategy. Document the result instead of making multiple changes simultaneously.
Example
A 6 mm end mill with 30 mm stick-out behaves differently from the same tool at 15 mm stick-out. Even if RPM and chip load remain identical, the longer setup may deflect and chatter more. The calculator cannot detect that difference.
Runout and uneven loading
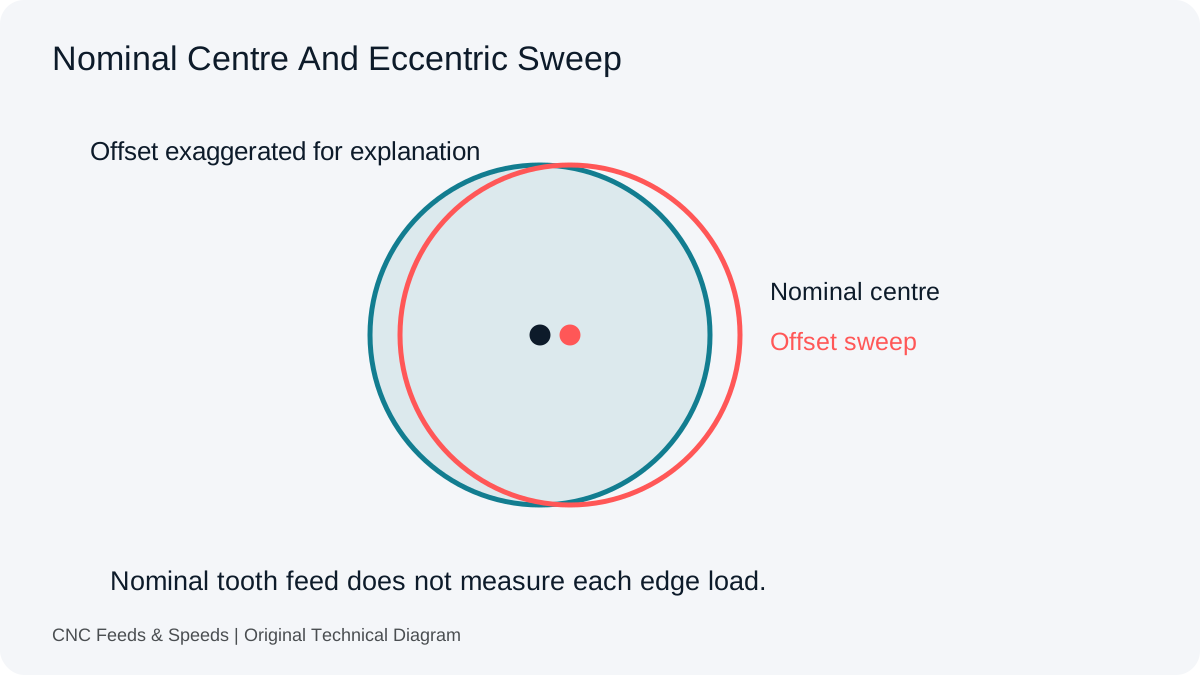
Radial runout can cause one flute to carry more load than another, effectively changing the chip distribution. This can produce chatter or accelerated wear even when the programmed feed and flute count are correct.
Workholding and part stiffness
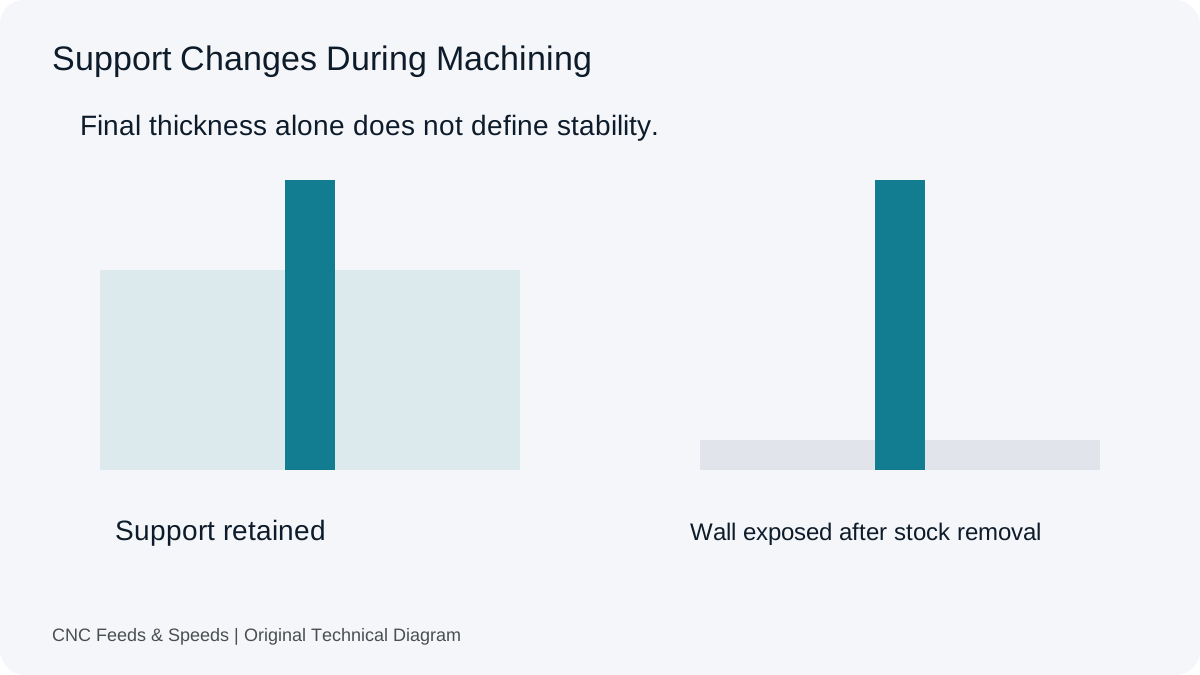
Thin walls, tall bosses, unsupported plates and flexible fixtures can transmit vibration into the cutter. Sometimes the right corrective action is a fixture or support change rather than a feed change.
Chatter troubleshooting order
Check tool reach, holder condition, runout, workholding, spindle/load behavior, engagement, tool geometry and cutting data. Make one deliberate change, then evaluate the result.
Document the stable condition
Record stick-out, holder, tool, material, RPM, feed, engagement, coolant and the stable result. This creates a process record that is more useful than simply saving a new feed rate.
Frequently asked questions
Can a calculator prevent chatter?
No. It can provide the arithmetic for cutting parameters, but chatter is a physical stability issue involving the complete machine-tool-workpiece system.
Is shorter stick-out always better?
Shorter is generally stiffer, but it must still provide the required access and clearance.
Should RPM always be reduced when chatter occurs?
Not automatically. Diagnose the system and apply a controlled stability adjustment appropriate to the toolpath and tooling data.
Applications And Related Calculation Workflows
Keep Calculation Errors Separate From Chatter Diagnosis
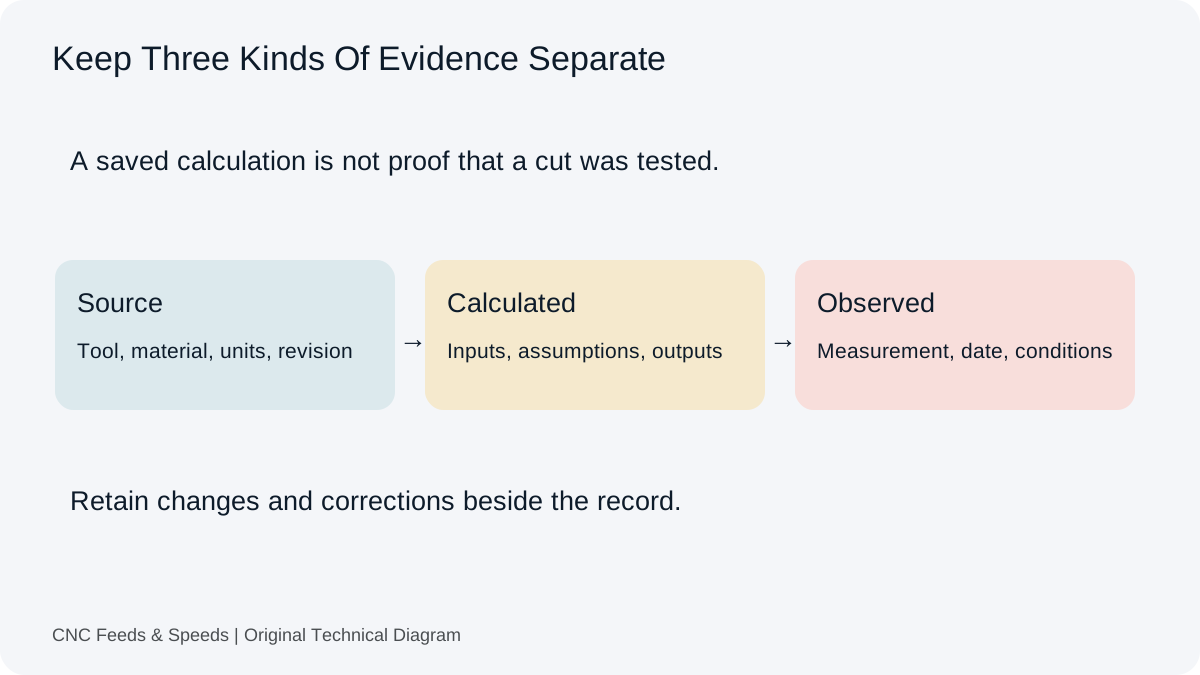
First verify the programmed RPM, feed convention and units against the source inputs. If the arithmetic is correct, it does not rule out a stability problem. Record tool reach, holder, engagement and workholding alongside the observed finish and sound so a change can be evaluated. The milling reference connects these setup variables without presenting a calculator as a chatter prediction model.
Related reading: Sandvik Coromant’s modular-tooling guidance discusses overhang, assembly length and stability. Its product-specific recommendations do not establish limits for every tool assembly. This article does not provide a measured stability chart or predict a chatter-free spindle speed.
Help Improve This Resource
Request A Tool
Describe the calculation your workflow needs, the inputs you already have and the output you want to check. Include units and an example without confidential job details.
Request A ToolReport An Error
Share this page address, the entered values and the result you expected. Include the source of your comparison so the formula, units and explanation can be investigated.
Report An ErrorCNC Feeds & Speeds Editorial Desk
The site brings calculation tools and machining references into one workspace. Use the editorial and site information to understand its purpose and limitations. Send corrections with a reproducible example through the error report form.