
Request A Tool
Describe the calculation your workflow needs, the inputs you already have and the output you want to check. Include units and an example without confidential job details.
Request A ToolConvert a known cutting speed into RPM using the effective cutting diameter. This is a rotation calculation, not a material recommendation. Enter cutter diameter for milling or drilling and workpiece diameter for conventional turning.
Convert a known cutting speed into RPM using the effective cutting diameter. This is a rotation calculation, not a material recommendation. Enter cutter diameter for milling or drilling and workpiece diameter for conventional turning. Keep the diameter and source cutting-speed units visible when comparing two setups, especially if one tooling chart uses inches and the other uses millimetres.
Check cutting speed and the diameter at the cutting edge.
Metric: RPM = 1000 × Vc ÷ (π × D). Imperial: RPM = 12 × SFM ÷ (π × D).
Enter the values you know. The result is calculated in your browser.
Calculation only. Verify toolmaker data, material grade, engagement, machine limits, workholding and actual cutting conditions before production.
Review the additional variables shown in this tool.
Enter the values you know. The result is calculated in your browser.
Calculation only. Verify toolmaker data, material grade, engagement, machine limits, workholding and actual cutting conditions before production.
Metric: RPM = 1000 × Vc ÷ (π × D). Imperial: RPM = 12 × SFM ÷ (π × D).
An illustrative cutting speed of 100 m/min and diameter of 10 mm give 3,183 RPM. At 20 mm, the same cutting speed gives 1,592 RPM. Doubling diameter halves RPM when cutting speed is held constant.
The shank diameter is not always the cutting diameter. For a rotating workpiece, a change in machined diameter changes the relationship between RPM and surface speed. Check which diameter the toolmaker formula expects.
A spindle ceiling changes actual cutting speed. With 10 mm diameter and a 2,000 RPM ceiling, actual speed is about 62.8 m/min. Check whether that condition is appropriate rather than treating the cap as a machining recommendation.
Check the formula reference or report a result that does not match your calculation.
Illustrative arithmetic only. Select cutting inputs from the applicable tool and material reference.
| Step | Substitution | Result |
|---|---|---|
| RPM | 1000 × 100 ÷ (π × 10) | 3,183.10 RPM |
RPM varies inversely with diameter. Entering a shank diameter where an effective cutting diameter is required changes the result even when the surface-speed input is correct. Keep full precision until the final RPM is chosen. The reverse cutting-speed calculation can check the surface speed at that command.
Formula reference: Sandvik Coromant milling formulas and definitions. Use the exact tool supplier for recommended cutting values.
RPM and spindle speed name the same rotational quantity in this calculation. A milling spindle speed calculation uses the cutter diameter; drilling uses drill cutting diameter. On a conventional lathe, use workpiece diameter at the cut. The CNC spindle speed formula remains a cutting-speed-to-diameter conversion rather than a decision about which cutting speed is suitable.
Check whether the calculated spindle speed is available on the actual machine. If a limit reduces RPM, calculate the resulting surface speed with the cutting speed calculator. For milling, recalculate linear feed from the actual RPM if you intend to preserve nominal feed per tooth. A numerical ceiling does not establish a suitable cutting condition.
In this calculation they describe the same result (revolutions per minute). Surface speed and diameter are the inputs. Feed rate is a separate quantity.
The actual surface speed is lower. The advanced panel shows that surface speed at the entered ceiling. Revisit the tool data and, for milling, recalculate feed using actual RPM.
Describe the calculation your workflow needs, the inputs you already have and the output you want to check. Include units and an example without confidential job details.
Request A ToolShare this page address, the entered values and the result you expected. Include the source of your comparison so the formula, units and explanation can be investigated.
Report An ErrorThe site brings calculation tools and machining references into one workspace. Use the editorial and site information to understand its purpose and limitations. Send corrections with a reproducible example through the error report form.
Continue with the calculation, setup or troubleshooting question closest to your task.
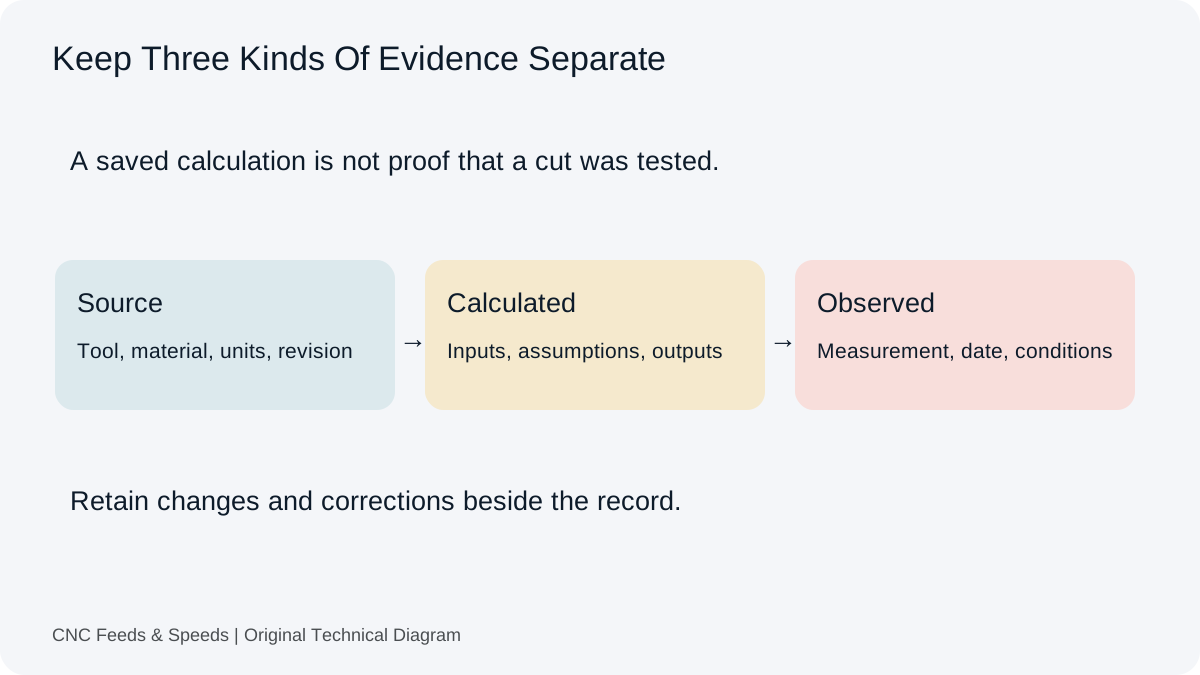
Preserve source data, calculated commands and observed results separately. Use local setup records with clear revisions, units and export limits.
Read Article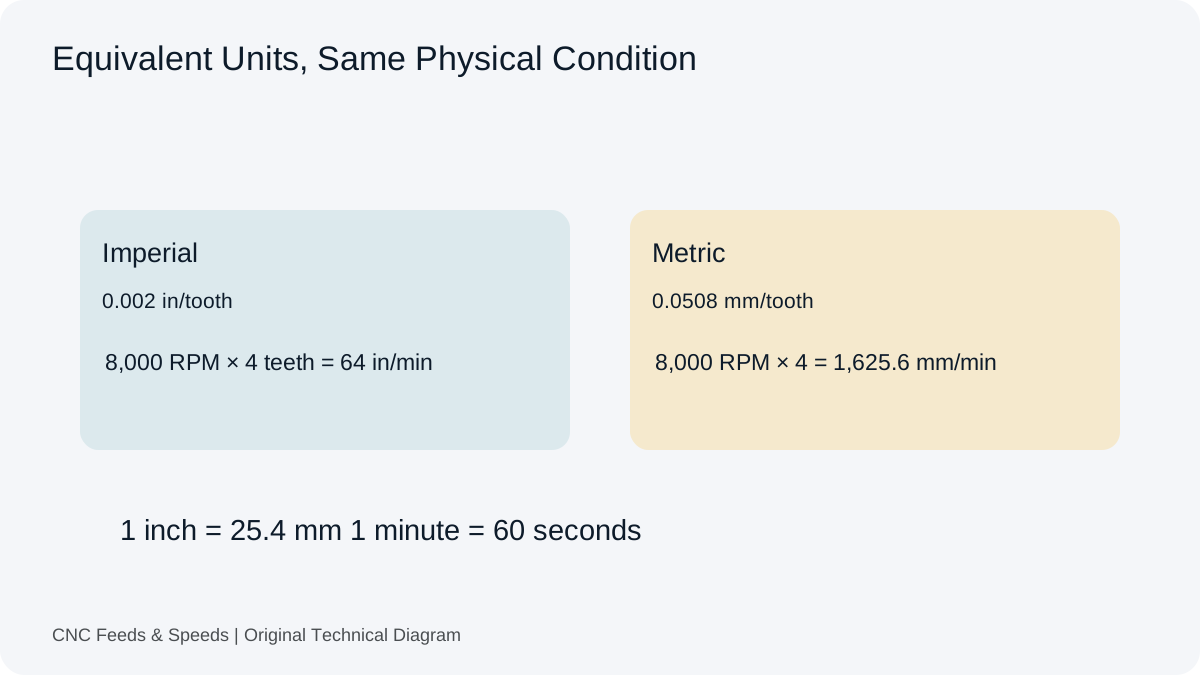
Check length, feed, surface speed, volume and pitch conversions. Follow equivalent metric and imperial examples before transferring a command.
Read Article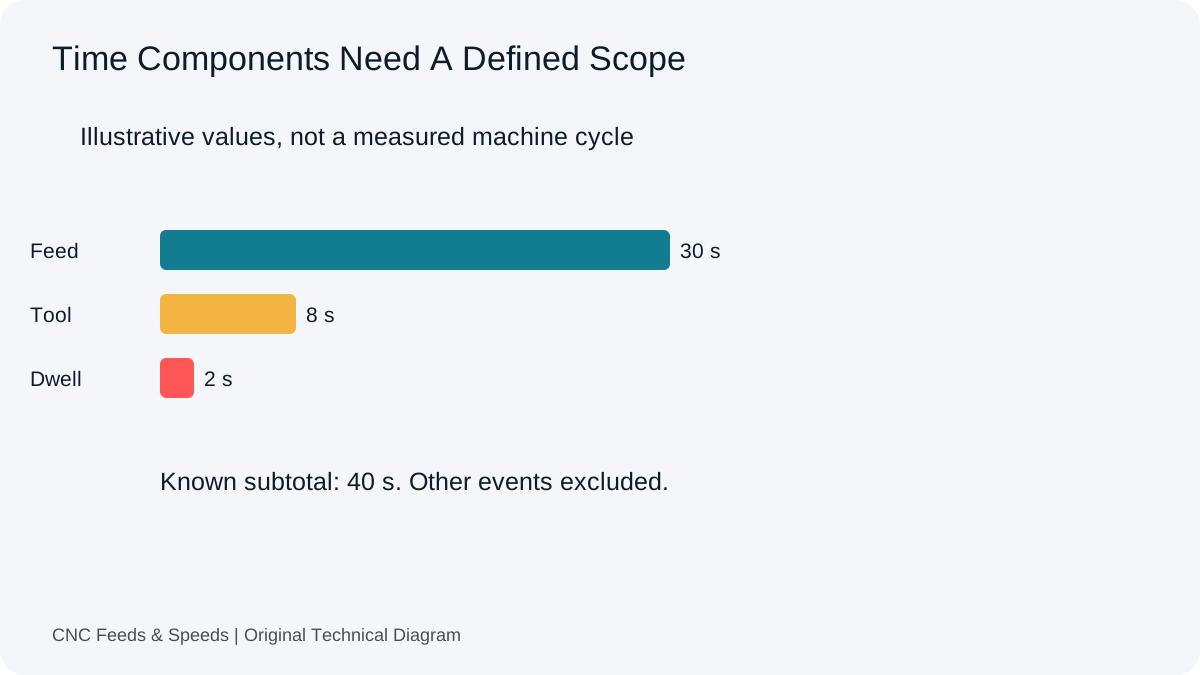
Define the scope behind each time figure. Separate feed travel, machine events, observations and production work before using an estimate.
Read Article
A practical method for interpreting CNC cutting-data charts, matching units, and cross-checking chart values with transparent calculations.
Read Article
Understand how spindle RPM and programmed feed interact, when feed should scale, and why machine limits change the calculation.
Read Article
Learn what surface feet per minute means, how it relates to RPM and diameter, and when to use SFM versus metric cutting speed.
Read Article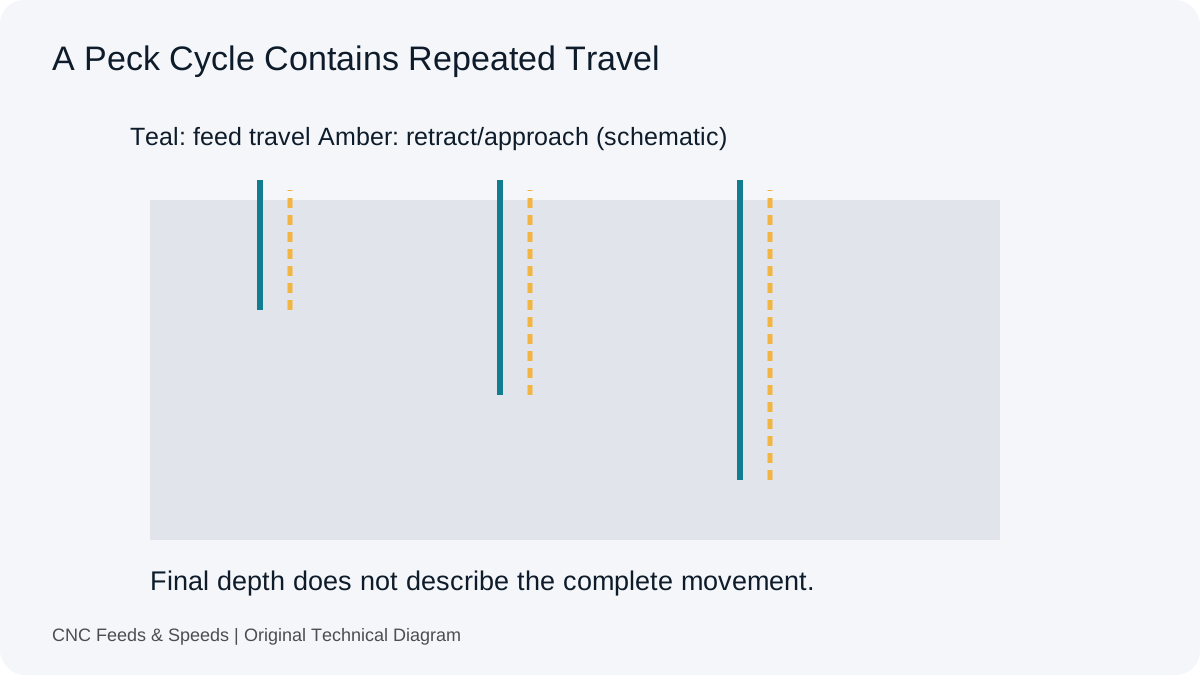
Separate new cutting travel, re-entry, retracts and dwell. Build a transparent time estimate that respects the actual cycle and controller.
Read Article
A practical guide to calculating CNC milling feed rate from spindle speed, flute count and chip load, with unit checks and verification steps.
Read Article
Understand feed per tooth, how chip load is calculated, and how flute count and spindle speed change milling feed.
Read Article
Calculate and interpret material removal rate for CNC milling, including feed, radial engagement and axial depth.
Read Article
Build an aluminum milling starting point from toolmaker cutting speed and chip load, then verify engagement, chip evacuation and machine limits.
Read Article
A calculation-first framework for stainless steel machining that emphasizes tool data, chip thickness, rigidity and heat control.
Read Article