Carbide and high-speed steel (HSS) tools use the same basic RPM and feed relationships, but their source cutting data can differ. Identify the actual substrate, geometry and coating before comparing values. A shared diameter does not make two tool specifications interchangeable.
Tool material is part of the cutting condition
A cutter diameter alone does not define the process. The substrate, grade, coating and geometry establish what cutting-speed and chip-load ranges are appropriate. Use the exact toolmaker information whenever possible.
Carbide context
Carbide commonly supports higher cutting speeds than HSS in applications for which the tool geometry and machine are suited. That does not mean every carbide cutter should be run at the maximum published value. Machine rigidity, runout, reach and engagement still constrain the process.
HSS context
HSS is valued for toughness, sharp edges and applications where the machine or setup is not suited to carbide conditions. Its appropriate cutting-speed range is generally different from carbide, and the feed must be calculated from the selected RPM and chip-load or feed-per-revolution data.
Worked arithmetic
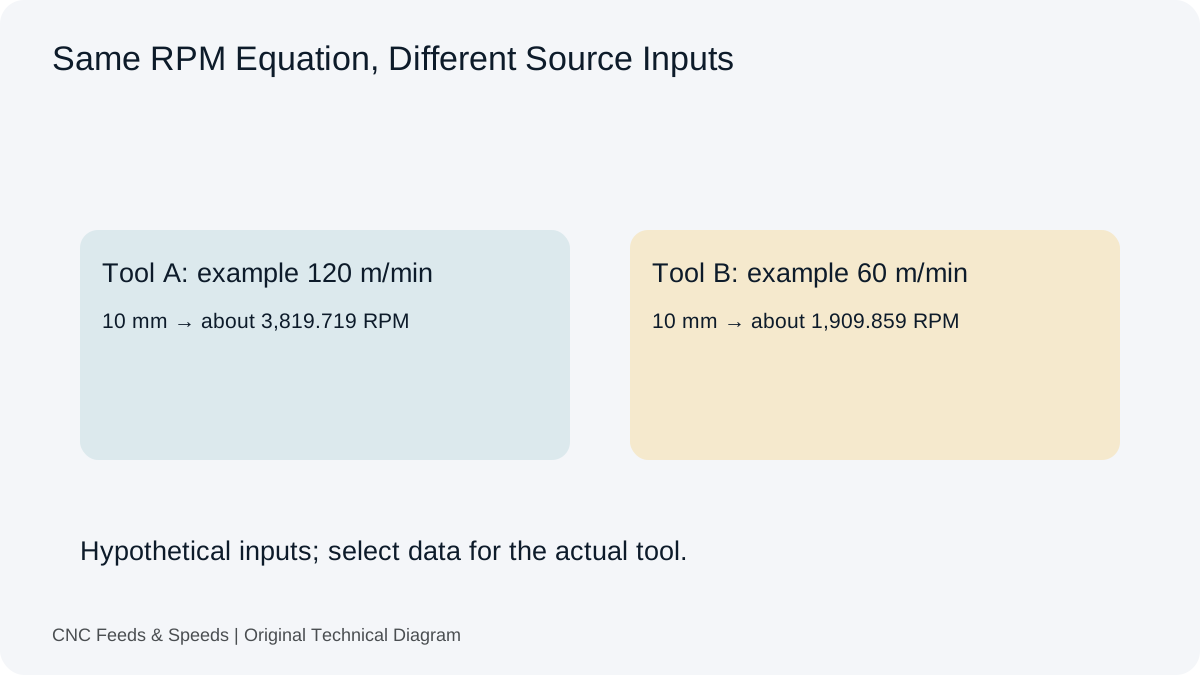
If a 10 mm cutter uses 120 m/min cutting speed, RPM ≈ 3,820. If another tool in the same operation uses 60 m/min, RPM ≈ 1,910. The calculator makes the difference explicit. The important choice is which cutting-speed source belongs to the actual tool.
Coating and geometry
Coating, helix, edge preparation and flute design can change cutting performance within the same base tool material. Read the product-specific chart rather than assuming all carbide tools use one set of values.
Machine stiffness
A faster tool is not automatically better if the machine or holder cannot maintain stability. High-speed cutting conditions can expose imbalance, runout or weak workholding more quickly.
Chip load still matters
Tool material does not remove the need to manage chip thickness. Once RPM is determined, calculate feed using the intended chip load and flute count for milling. For turning or drilling, use the operation-specific feed convention.
Heat management
Carbide and HSS handle heat differently, but coolant and chip evacuation remain process variables. A calculator cannot determine whether a coolant strategy is adequate.
Choosing between them
Select tool material based on the feature, material, production demand, machine capability, rigidity and tooling availability. Record the chosen tool and actual cutting data so future jobs can be compared fairly.
Frequently asked questions
Can I use a carbide chart for HSS?
No. Use cutting data for the actual tool construction and geometry.
Does carbide always mean higher RPM?
It can support higher cutting speeds in many applications, but the machine, tool geometry and material determine the appropriate range.
Do carbide and HSS use different feed calculations?
The underlying milling feed equation is the same; the tool-specific chip load and cutting-speed inputs are different.
For a producer example of tool choice tied to a specified material application, see SSAB’s machining questions. Apply its instructions only within the stated product and machine conditions.
Help Improve This Resource
Request A Tool
Describe the calculation your workflow needs, the inputs you already have and the output you want to check. Include units and an example without confidential job details.
Request A ToolReport An Error
Share this page address, the entered values and the result you expected. Include the source of your comparison so the formula, units and explanation can be investigated.
Report An ErrorCNC Feeds & Speeds Editorial Desk
The site brings calculation tools and machining references into one workspace. Use the editorial and site information to understand its purpose and limitations. Send corrections with a reproducible example through the error report form.